Conveyors

Industrial Conveyor Systems & Automated Material Handling

What purpose do conveyors have? A conveyor system's main purpose is to move products efficiently and safely from one location to another. The industrial designs manufactured by CM Machine Services allow for the seamless mobility of products that are too heavy, too bulky, too fragile, or simply require mechanical transport to uphold strict hygienic food transfer processes.

By eliminating manual labor bottlenecks and optimizing factory workflows, our advanced conveyor systems save time, drastically reduce product giveaway, and increase overall facility profitability.

High-Performance Automation for Intralogistics and Packaging Lines

A frequently asked about piece of equipment in our lineup is the high-precision Automatic Tray Loading Conveyor. This advanced system moves products from a former or feeding line automatically without harming delicate food profiles. It achieves this by lowering the tray and retracting the belt and conveyor with extreme precision and high performance. Because of its capability to move vast volumes of goods within a limited amount of time, it is ideally suited for high-production packaging facilities.

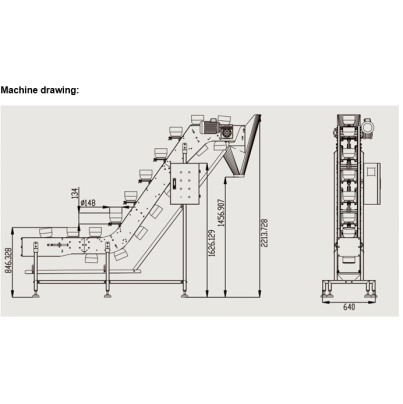
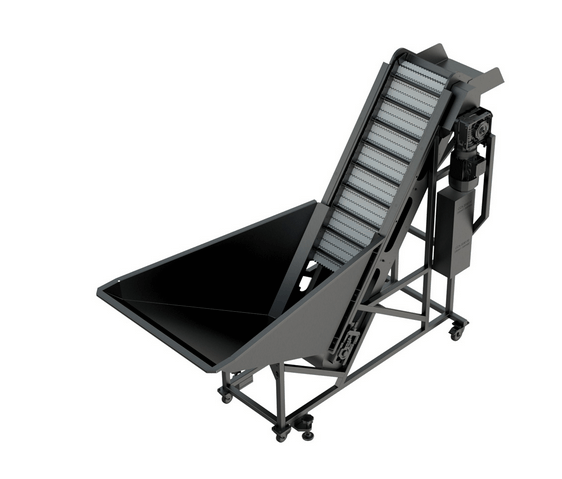
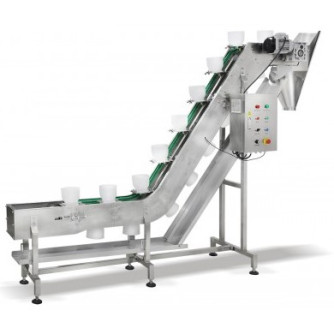
For specialized product routing, another commonly asked about piece of equipment is our Bowl Type Conveyor. This system is uniquely engineered to convey solid, granular, or small-sized products upwards into fillers or multi-head weighers. In the past, it was heavily relied upon as a secondary lifting solution due to the tight constraints of plant field space, ensuring maximum vertical incline efficiency without a massive floor footprint.

Sanitary Design & Line Integration Highlights

In the process of achieving optimal line efficiency with low long-term operational costs, all of our conveyors play important roles within operations ranging from small startups to large processing plants:

  • Hygienic Food-Grade Belting: Equipped with chemical-resistant, washdown-safe modular belts or homogeneous polyurethane belts to prevent bacterial harborage.
  • Gentle Product Handling: Precision retraction and lowering mechanisms prevent product shifting, marking, or cosmetic damage during high-speed transfers.
  • Space-Optimized Elevators: Pocket-belt, bucket, and bowl-style configurations engineered to cleanly elevate ingredients over existing equipment lines.
  • Heavy-Duty Stainless Steel Frames: Built with open-frame stainless steel construction to simplify daily sanitation cycles and satisfy rigorous regulatory audits.
  • Synchronized Line Controls: Smart sensor arrays allow the conveyor to communicate with upstream forming machinery and downstream packaging units smoothly.
  • Comprehensive Engineering Support: Full design collaboration from CM Machine Services to match layout lengths, belt widths, motor speeds, and incline angles to your exact footprint.

Optimize Your Product Transfer Efficiency

Whether you need an inline tray loader to feed an automatic thermoformer or a vertical elevator to transport bulk granular ingredients, our systems are built to deliver uncompromised reliability. Contact the engineering specialists at CM Machine Services today to analyze your product dimensions, line velocities, and floor space to build the perfect conveyor solution.

...Read less (-)
Industrial Conveyor Systems & Automated Material Handling What purpose do conveyors have? A conveyor system's main purpose is to move products efficiently and safely fro... Read more (+)
Brand: CM Machine Services Stock: On Order
Belt Conveyor The belt conveyor is completely customizable. Measurements of the Width, Length, and Height are needed to create the conveyor to m..
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
Bowl Type Conveyor Applicable for lift-conveying of solid, granular, small-sized products, and more often for secondary lifting solution due to..
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
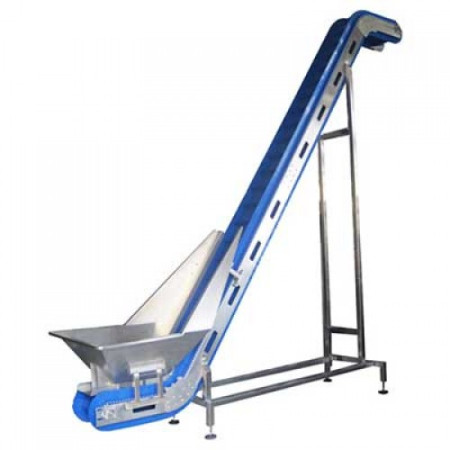
Bucket Conveyor Conveyor belts are the most essential part of any production line. CM Machine offers a wide range of customized conveyor belts...
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
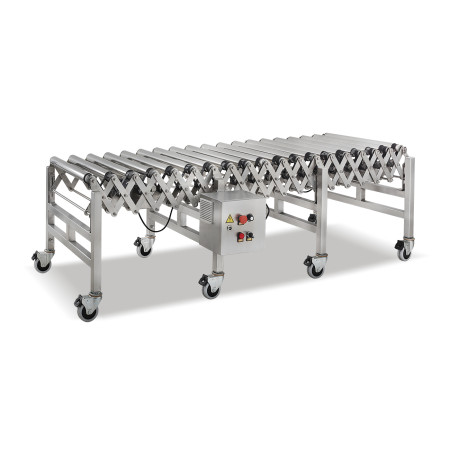
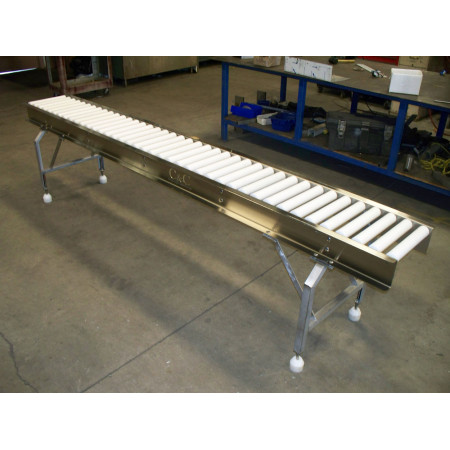
Extendible Roller Conveyor Applicable for conveying packed products in boxes/bags or on trays/containers (for bulk cargo, smaller, or irregular sha..
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
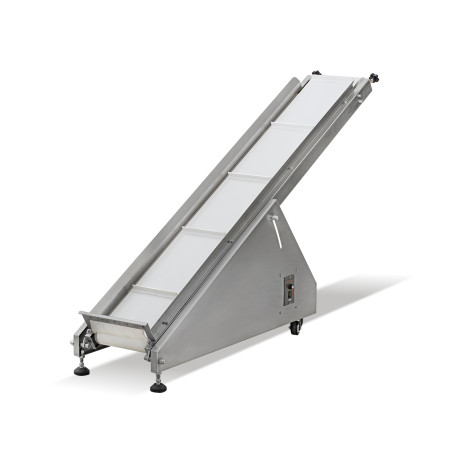
Finished Product Conveyor Mainly used to undertake packaged products and convey them to the weight checking/metal detecting equipment or packing pl..
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
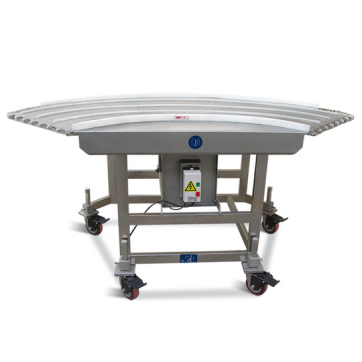
Finished Product Conveyor Mainly used to undertake packaged products and convey them to the weight checking/metal detecting equipment or packing pl..
View Details
Request Quote
Brand: CM-HM-CN Stock: On Order
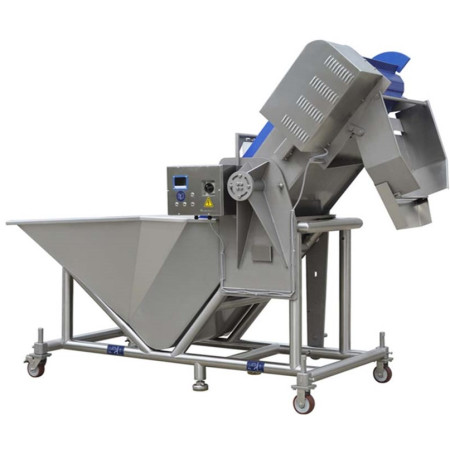
Food Grade 90° Conveyor This conveyor is efficient in conveying the food products to the next processing position by 90°. Ip65 waterproof rating..
View Details
Request Quote
Brand: CM-HM-CN Stock: On Order
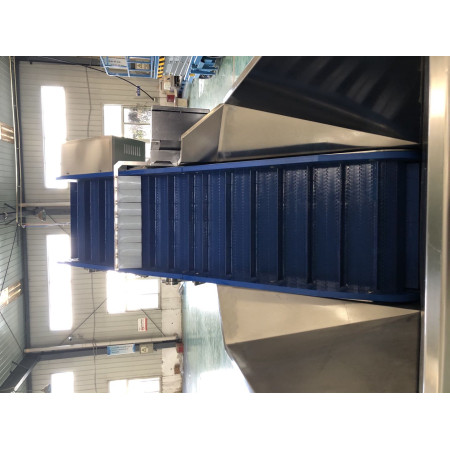
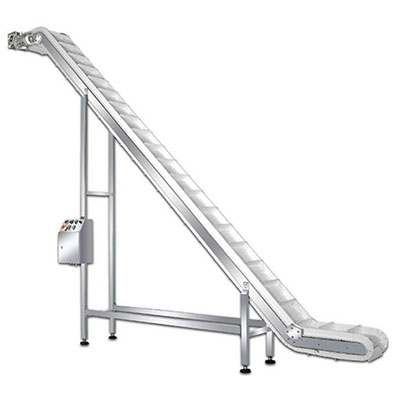
Inclined Bulk Conveyor Inclined Bulk Conveyor is designed for transferring bulk food, particularly for boneless and bone-in products, the meat proc..
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
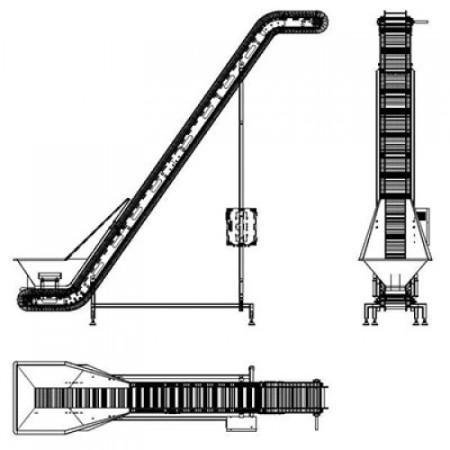
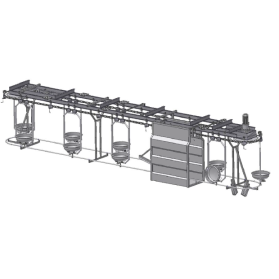
Inclined Conveyor Applicable for lift-conveying of granular products such as potato chips, candies, nuts, frozen food, vegetables, chemical medicin..
View Details
Request Quote
Brand: 1228 Stock: On Order
Plate Conveyor for Intestines (Pig Slaughterhouse) This conveyor is designed for transporting intestines and centers from one station to the other...
View Details
Request Quote
Brand: CM Machine Services Stock: On Order
Roller Conveyors These conveyors are designed to move and hold products while adding flexibility to your processing line. There’s the option of..
View Details
Request Quote
Brand: CM-TP-CN Stock: On Order
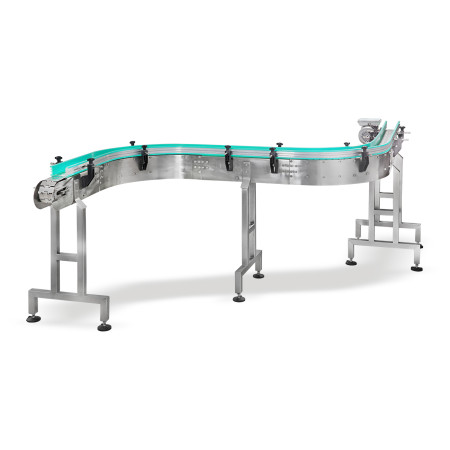
S-Type Conveyor for Food Plants This conveyor is an automatic conveying machine. Main Functions and Features: Distribution of bottled,..
View Details
Request Quote
Showing 1 to 12 of 18 (2 Pages)